-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog
Why Choose an Industrial Foiling Machine?
Why Choose an Industrial Foiling Machine?
In modern packaging and print production, surface appearance can influence perceived quality within seconds. An Industrial Foiling Machine applies metallic, colored, or specialty foil with controlled pressure and heat. This process creates sharp lettering, reflective panels, and consistent decorative details across large production runs. It is especially useful for cartons, labels, book covers, luxury packaging, and promotional materials. A well-configured system can improve throughput while reducing manual finishing work. It can also support repeatable results when operators monitor temperature, pressure, foil tension, and material alignment. Small adjustments matter.
The practical value extends beyond visual appeal. Automated foil application may reduce setup waste and improve registration accuracy compared with slower manual methods. Modern equipment can integrate with feeding, stamping, embossing, and inspection systems. This integration helps manufacturers maintain stable workflows and document quality checks. However, purchasing one is not automatically the right decision. An industrial machine requires floor space, trained operators, regular maintenance, and suitable ventilation or safety controls. Energy use and foil consumption also deserve careful review. The cheapest model may become expensive when downtime and replacement parts are considered. That assumption deserves scrutiny.
Choosing correctly means comparing production volume, substrate types, foil patterns, changeover time, and expected return on investment. Experienced suppliers should provide technical specifications, sample testing, service support, and realistic performance data. Ask difficult questions. Can the machine handle your actual materials? Will operators receive practical training? A careful evaluation helps businesses select equipment that delivers dependable finishing quality rather than impressive promises.
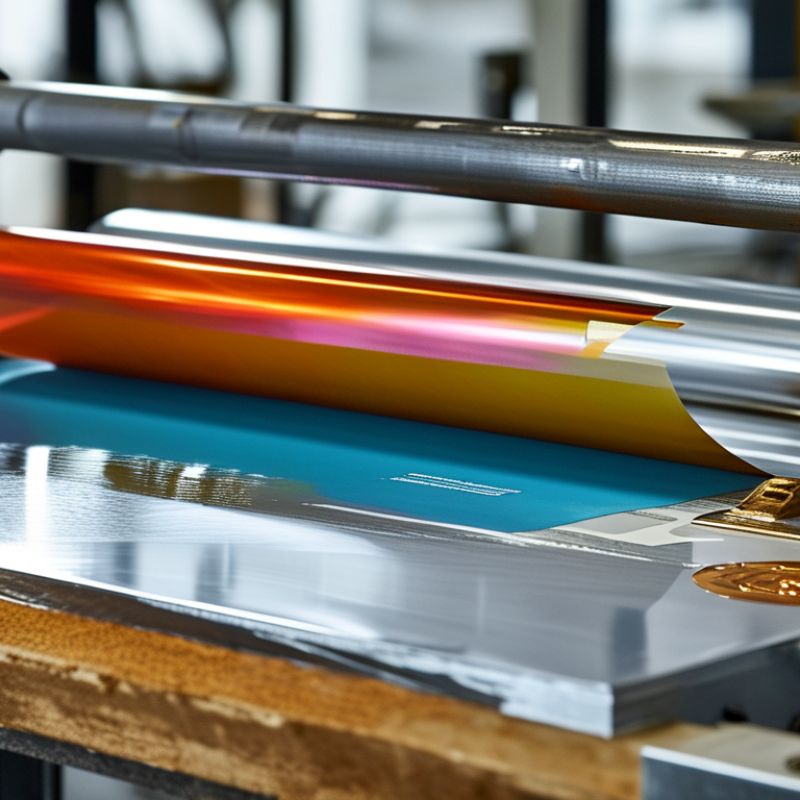
Table of Contents [Hide]
What Is an Industrial Foiling Machine?
An industrial foiling machine is production equipment that applies thin metallic or colored foil to printed materials. It uses controlled heat, pressure, and a heated die or patterned cylinder to transfer the foil. Depending on its design, it may process labels, cartons, covers, tags, or flexible packaging at high speed. The foil unwinds from a roll, while sensors help align each impression with the printed surface. That alignment matters.
In a typical operation, an operator loads the substrate, selects temperature, adjusts pressure, and sets feed speed. The machine then presses the foil against the material for a measured time. Heat activates the foil’s release layer, while pressure bonds its pigment or metallic finish to the surface. Modern systems may include registration controls, waste monitoring, and automatic tension adjustment. These features reduce variation, but they do not replace skilled observation. A small wrinkle, dull patch, or uneven edge can reveal incorrect settings.
From hands-on production, the difficult part is often matching foil, substrate, and artwork. Coated paper may respond differently from textured board or synthetic film. Humidity, surface dust, and die wear can also affect the result. Industrial foiling is efficient, yet it is not completely automatic. Good results depend on testing, maintenance, and careful inspection under normal lighting. I would not treat the first successful sample as proof of a perfect setup. Repeated checks are wiser.
Why Choose an Industrial Foiling Machine? - What Is an Industrial Foiling Machine?
A practical overview of industrial hot foil stamping equipment, typical operating capabilities, and key selection criteria.
Note: Operating ranges are representative industry ranges rather than universal specifications. Actual performance depends on machine configuration, die design, foil construction, substrate properties, artwork coverage, and production conditions.