-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog
China Top Micro Injection Mold Manufacturers?
Finding China’s top Micro Injection Mold manufacturers requires more than browsing polished factory websites. A reliable evaluation should examine mold precision, material knowledge, production controls, and communication during difficult projects. Tiny medical, electronic, and optical parts can expose weak tooling quickly. Flash, short shots, uneven cooling, or damaged ejector pins may appear after only a few cycles.
Experienced buyers should review actual workshop evidence. Look for CNC machining centers, precision grinding, electrode manufacturing, and controlled inspection areas. Ask for tolerance reports, steel certificates, mold-flow analysis, and sample parts from comparable projects. A serious supplier should explain cavity design, gate placement, venting, shrinkage, and expected mold life in clear language. ISO certification can support confidence, but it should not replace an onsite audit or independent verification.
The best manufacturer depends on your application, not advertising language. Medical components may require traceability and documented validation. Micromechanical parts may demand optical measurement and stable molding conditions. Export experience also matters, especially when drawings, packaging, and technical approvals cross borders. No ranking is perfect. Supplier capabilities change, and some impressive samples hide weak after-sales support. That is why this guide compares practical evidence, communication quality, engineering depth, and customer feedback. It aims to identify manufacturers that can build consistent Micro Injection Mold solutions, not merely attractive prototypes. A careful shortlist still needs testing. Request a detailed quotation, inspect trial parts, and confirm corrective-action procedures before placing a major order.
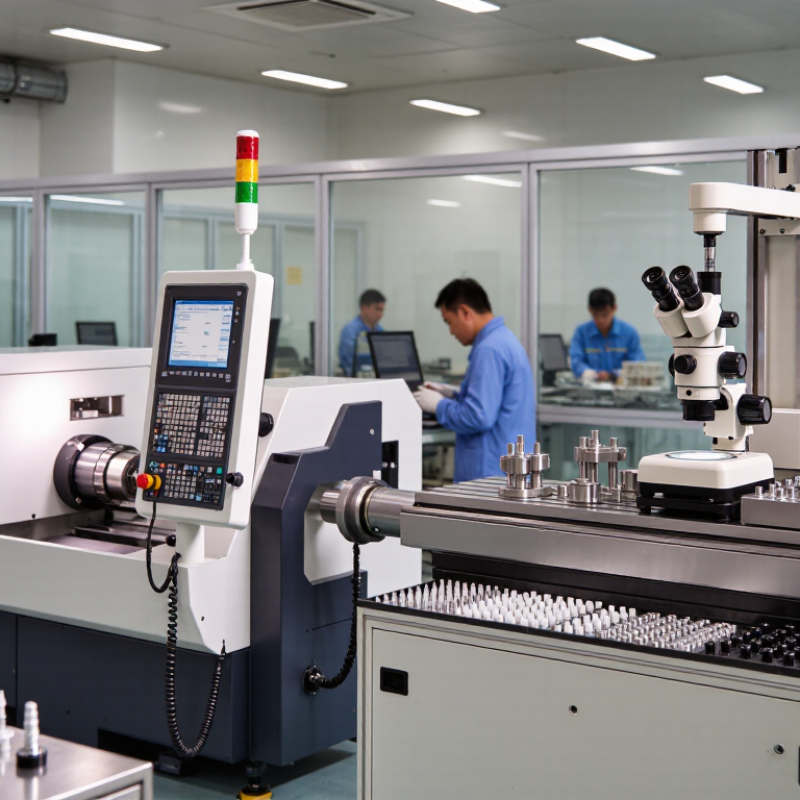
Table of Contents [Hide]
Micro Injection Molding Defined: 0.01–1 mm Features and ±0.005 mm Tolerance
Micro injection molding produces parts with features from 0.01 to 1 mm. It is used for miniature medical, optical, electronic, and laboratory components. At this scale, a small burr can block a channel or change fluid movement. The process is not simply ordinary molding made smaller.
A capable manufacturer studies resin behavior, mold steel, gate location, and cooling balance together. A 0.01 mm rib may require polished tooling and carefully controlled filling speed.
Achieving ±0.005 mm tolerance also demands stable machines, dry material, and temperature control. Measurement should combine optical systems, microscopes, and calibrated dimensional equipment. One measurement is not enough. Process data matters.
Experienced teams also inspect the mold before production begins. They check vent depth, cavity alignment, ejector movement, and tool wear. Some materials shrink unpredictably, especially after moisture exposure. That reality can defeat an impressive drawing.
Perfect repeatability is difficult. A better approach is to validate critical dimensions through pilot runs and capability studies. Manufacturers should explain their measurement method, sampling plan, and acceptable variation clearly. They should also provide traceable inspection records, not only attractive sample parts.
Designers may need to reconsider tolerances when function allows it. Tighter is not always better. It can increase tooling time, scrap, and cost without improving performance.