-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog
China Top Pouch Cell Trimming Machine Suppliers?
China has become an important sourcing base for pouch battery production equipment. This guide examines China’s top Pouch Cell Trimming Machine suppliers through practical purchasing criteria. The focus is not only on catalog claims. It considers trimming accuracy, sealing-edge quality, machine stability, and service capability.
A reliable supplier should explain how its equipment handles different pouch sizes, film thicknesses, and production speeds. Buyers should request sample trials using their own cells. Watch the trimmed edges closely. Uneven cuts, loose film, metal particles, and repeated positioning errors can affect later assembly steps. Servo control, adjustable tooling, dust management, guarding, and changeover time also deserve careful review. A clear acceptance test is essential.
Experience matters here.
Factory visits can reveal details that brochures omit. Check assembly quality, spare-parts storage, software support, operator training, and documented inspection records. Ask for references from comparable battery projects, not unrelated machinery installations. Safety design, electrical documentation, traceability, and compliance support should be verified for the intended market. Supplier rankings can change as technology and service teams develop. A polished presentation cannot replace performance data.
No supplier is perfect. Some manufacturers may offer excellent cutting precision but limited overseas support. Others may provide responsive service while needing stronger customization experience. This article therefore presents a balanced framework for comparing China-based suppliers. It helps engineering teams identify a suitable Pouch Cell Trimming Machine through evidence, testing, and realistic production requirements, rather than price alone.
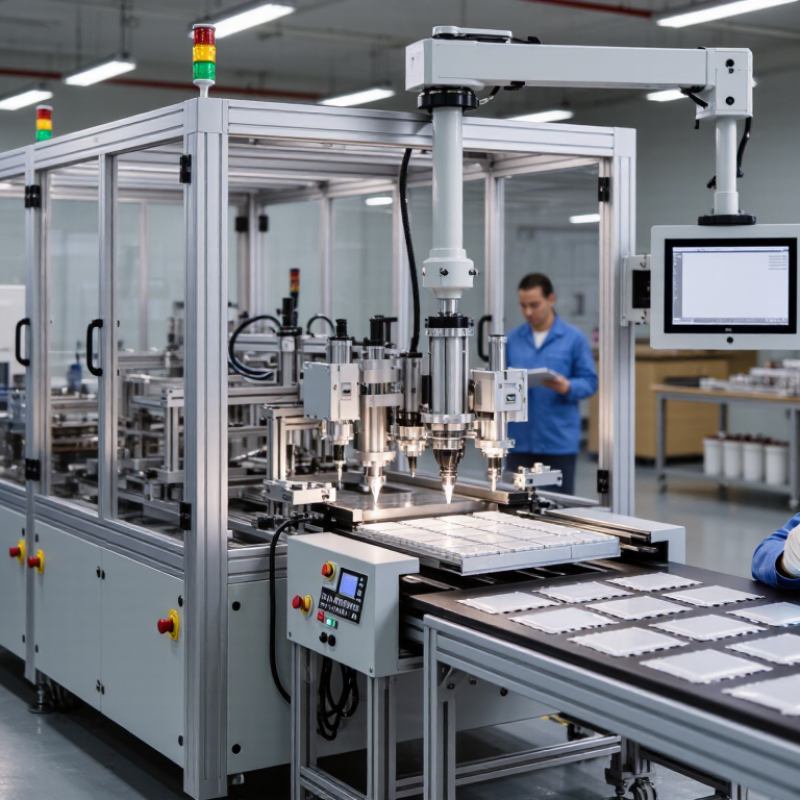
Table of Contents [Hide]
What Is a Pouch Cell Trimming Machine?
A pouch cell trimming machine removes excess aluminum-plastic film after the cell has been heat-sealed. It creates a clean, consistent edge around the battery pouch. It is precise work. The process can use guided blades, dies, or servo-driven cutting tools. Sensors help position each cell before trimming begins.
In a typical production line, an operator loads sealed cells onto a fixture. The machine clamps the pouch without crushing its soft body. A cutting unit then follows a programmed path and separates unwanted film. Dust collection, guarding, and interlocks help protect workers and reduce contamination. Small errors matter. A few millimeters of uneven trimming may affect later folding, insulation, or module assembly.
Reliable equipment should provide adjustable cutting pressure, stable positioning, and repeatable results across different cell sizes. Engineers should check edge quality under magnification and measure trimmed dimensions regularly. In my experience, trial samples reveal problems that specifications can miss. Film thickness, sealing temperature, and pouch deformation can change the final result. No setup is perfect. A careful supplier should support sample testing, maintenance guidance, spare cutting parts, and clear acceptance criteria. Some machines appear fast but produce rough edges during continuous operation. That weakness deserves attention before installation.
China Top Pouch Cell Trimming Machine Suppliers? - What Is a Pouch Cell Trimming Machine?
Definition: A pouch cell trimming machine is an automated or semi-automated system used to remove excess pouch-film material from lithium-ion battery cells after forming, sealing, or related assembly processes. The machine is selected according to cell dimensions, film structure, trimming profile, production speed, and required edge quality.
Note: The technical values above are general industry reference ranges. Final specifications should be confirmed through sample testing because pouch-cell dimensions, laminate structures, sealing layouts, and production requirements vary by application.