-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog
China Top 10 PVC Profile Mixer Manufacturers
Choosing a Pvc Profile Mixer in China requires more than comparing motor power, vessel size, or catalogue prices. A reliable machine must disperse calcium carbonate, stabilizers, pigments, and PVC resin evenly. It should also protect the blend from overheating during repeated cycles. In a working factory, operators watch the temperature display closely. They check whether powder clings to the vessel wall. They listen for unusual vibration. These small details often reveal more than a polished brochure.
Dr. Michael Thielen, a plastics-processing specialist, offers a useful principle: “A mixer must deliver repeatable dispersion, not merely impressive speed.” This idea guides the China Top 10 PVC Profile Mixer Manufacturers review. The selection considers mixing uniformity, blade design, cooling performance, discharge structure, control systems, spare-parts support, and documented production experience. It also examines whether manufacturers can adapt machines for different profile formulations and batch sizes. A strong supplier should explain its testing method clearly. That matters.
No ranking is perfect. Buyer priorities differ. Some plants need compact equipment for flexible production. Others require high-volume systems with automated feeding and temperature control. Price can attract attention, but weak after-sales support may create longer costs later. We therefore compare practical evidence, including factory applications, technical documentation, customization ability, and service response. A few manufacturers may provide limited public data, which deserves caution rather than automatic rejection. This introduction is not a final verdict. It is a careful starting point for engineers, purchasing teams, and plant owners seeking a dependable Pvc Profile Mixer.
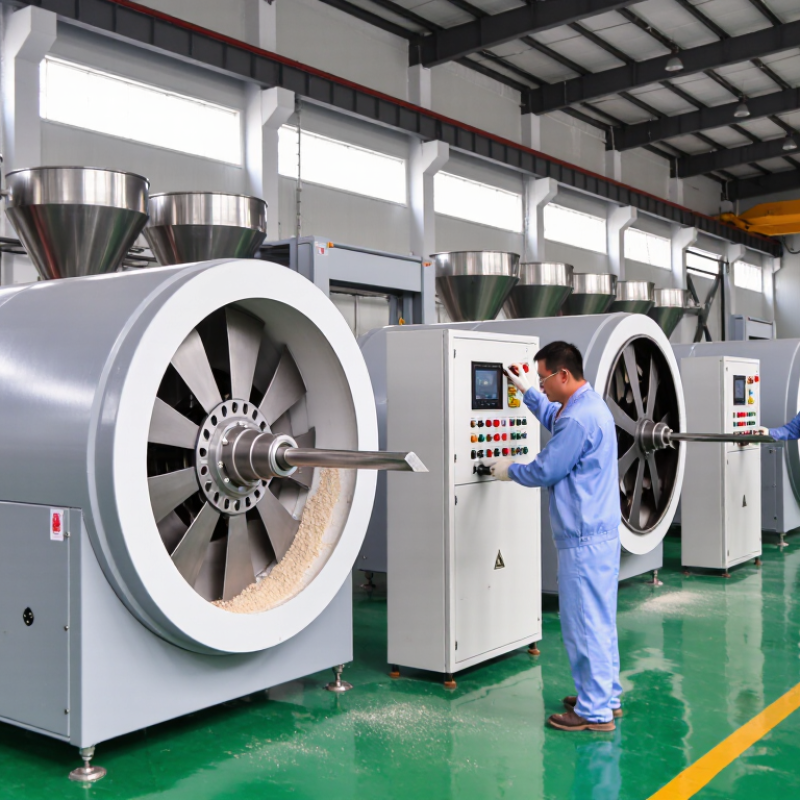
Table of Contents [Hide]
Definition and Role of PVC Profile Mixers in Plastic Manufacturing
A PVC profile mixer is an industrial machine that prepares a uniform compound before extrusion. It blends PVC resin with stabilizers, pigments, lubricants, fillers, and impact modifiers. The mixer does not simply stir materials. It controls heat, dispersion, moisture, and powder flow. These factors directly influence profile strength, surface quality, and dimensional stability.
In plastic manufacturing, the mixer usually combines high-speed heating with controlled cooling. During heating, friction helps distribute additives throughout the resin. A cooling stage then reduces material temperature before extrusion. This prevents premature fusion and reduces feeding problems. In production practice, operators monitor mixing time, blade speed, temperature, and batch weight. Small changes can create visible streaks or brittle edges. Clean equipment matters too. Residue from an earlier color can affect the next batch.
When assessing China’s top 10 PVC profile mixer manufacturers, buyers should examine process data rather than appearance alone. Useful evidence includes test reports, temperature records, spare-part support, and trial-batch results. A reliable supplier should explain how the mixer handles different formulations and output levels. Some specifications look impressive on paper. They may still fail under continuous operation. That is where careful testing is necessary. Operators should also review noise, dust control, energy use, and cleaning time. The best choice depends on the recipe, profile design, factory space, and production rhythm, not only the machine’s rated capacity.