-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog
China Best Metal Stamping Parts Manufacturer?
Choosing the best Metal Stamping Parts manufacturer in China requires more than comparing online prices. Real performance appears in the toolroom, inspection area, and production records.
A reliable supplier should understand progressive dies, deep drawing, precision blanking, and material springback. The factory should also provide traceable steel certificates, first-article inspection reports, and clear dimensional tolerances. Ask to see the presses. Observe the tooling. Notice whether operators check burrs, cracks, and surface marks during production.
Dr. Taylan Altan, a respected metal forming expert, stated, “Successful stamping depends on the interaction of material, tooling, and process.” That principle remains practical today. A strong manufacturer does not treat Metal Stamping Parts as simple pressed shapes. It studies the customer’s drawing, forming sequence, load requirements, and expected service life.
Some factories advertise impressive equipment but provide weak engineering support. That gap can create late deliveries, unstable dimensions, or expensive die repairs. I have seen small details matter: a poorly controlled pilot pin can shift a hole pattern, while excessive clearance can leave sharp edges.
Perfection should not be assumed. Even experienced suppliers can miss a tolerance or underestimate material variation. The better question is how quickly they identify and correct the problem. Look for documented corrective actions, process capability data, in-house tooling experience, and responsive communication.
The best choice is rarely the cheapest quote. It is the manufacturer that can repeatedly deliver safe, consistent, and application-ready Metal Stamping Parts. Reliability is built one inspection record at a time.
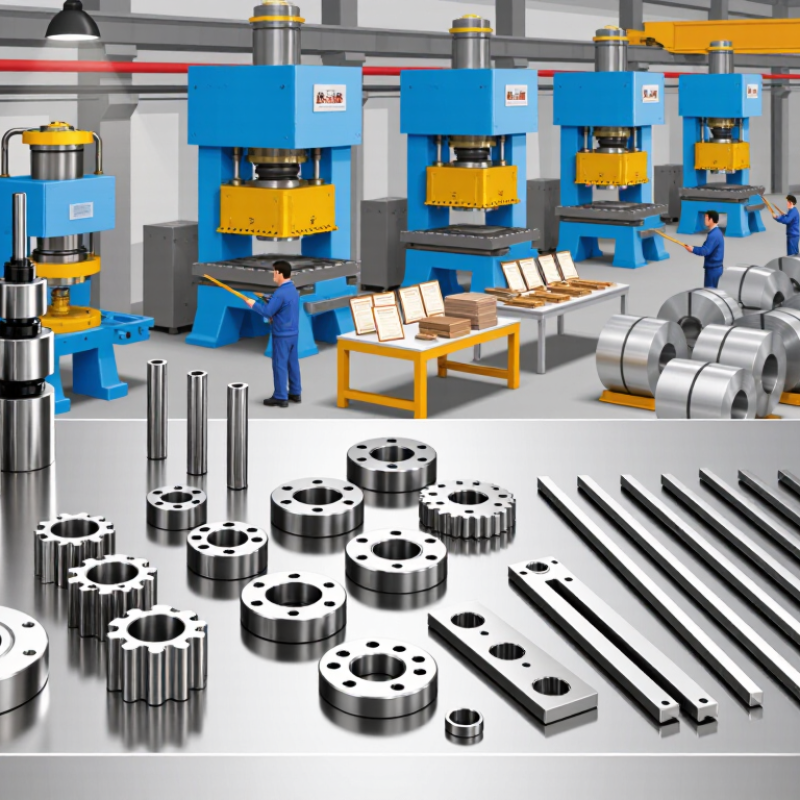
Table of Contents [Hide]
What Makes China’s Best Metal Stamping Parts Manufacturer?
What Makes China’s Best Metal Stamping Parts Manufacturer?
China’s best metal stamping parts manufacturer is not simply the lowest-cost supplier. It combines tooling experience, stable production, inspection discipline, and clear communication. Grand View Research valued the global metal stamping market at about USD 211.9 billion in 2023. This scale increases competition, but it also makes process control more important.
A capable manufacturer should explain material selection, die structure, press capacity, and tolerance limits before production begins. Look for incoming material checks, first-article inspection, SPC records, and batch traceability. ISO 9001 certification supports reliability, but certification alone proves little without usable inspection data. For automotive or electrical components, PPAP knowledge and Cpk monitoring can reduce hidden risks. A strong factory should also provide samples that match real production conditions, not carefully adjusted prototypes. That distinction is easy to miss.
Tips: Request a small pilot run. Measure burr height, flatness, hole position, and coating quality. Ask how rejected parts are isolated. Verify material certificates with the delivered batch. Confirm packaging before signing the order.
The best supplier also understands production pressure. It can suggest a radius change, a better steel grade, or a simpler forming sequence. These changes may reduce cracking and tool wear. Still, no manufacturer is perfect. Some factories communicate well but document poorly. Others show excellent equipment but weak follow-up. A practical audit should compare records, sample results, operator skills, and response speed. Price matters, but predictable quality matters more.