-
- Products
- Indoor Household Cords
- Appliance Cords
- General Purpose Short-Length Cords
- General Purpose Extension Cords
- Landscape & Decorating Cords
- Bright Color Extension Cords
- Oil-Resistant Extension Cords
- Cold-Flex Extension Cords
- VividFlex Power Cords
- EXTREME All-Weather Cords
- Cord Management
- Task Lights
- Adapters & GFCI Devices
- Where to Buy
- About
- Careers
- Glossary
- Catalog
What Is the Best Fusion Pipe Welder?
Choosing the best Fusion Pipe Welder requires more than comparing heating temperatures, clamp sizes, or advertised pressure ratings. A reliable machine must create consistent joints under real working conditions. That means stable heat, accurate alignment, strong hydraulic control, and clear operating feedback. It must also suit the pipe material, diameter range, job location, and production schedule.
Robert A. McElroy, founder of McElroy Manufacturing, is widely associated with modern thermoplastic pipe fusion equipment. His practical principle is often expressed this way: “A good fusion joint begins with preparation.” The idea remains relevant. Clean pipe ends, correct facing, proper bead formation, and controlled cooling can matter as much as the welder itself. Even the most advanced Fusion Pipe Welder cannot correct careless preparation.
Field experience exposes the difficult details. Mud can enter the facing area. Wind can cool the pipe surface too quickly. A crowded trench can make alignment awkward. These conditions separate a dependable machine from a merely impressive one. Look for durable frames, repeatable temperature control, readable gauges, and service support that responds quickly. Data logging is valuable, but it does not replace trained judgment.
There is no universal winner.
A compact hydraulic welder may be ideal for municipal repairs, while a large automated unit may suit long pipeline projects. Buyers should compare total ownership cost, operator training, maintenance access, and available fusion tooling. Some product reviews focus heavily on specifications. That is incomplete. The best Fusion Pipe Welder is the one that produces repeatable, verifiable joints when the site becomes inconvenient. Mistakes happen. Good equipment makes them easier to detect and less likely to repeat.
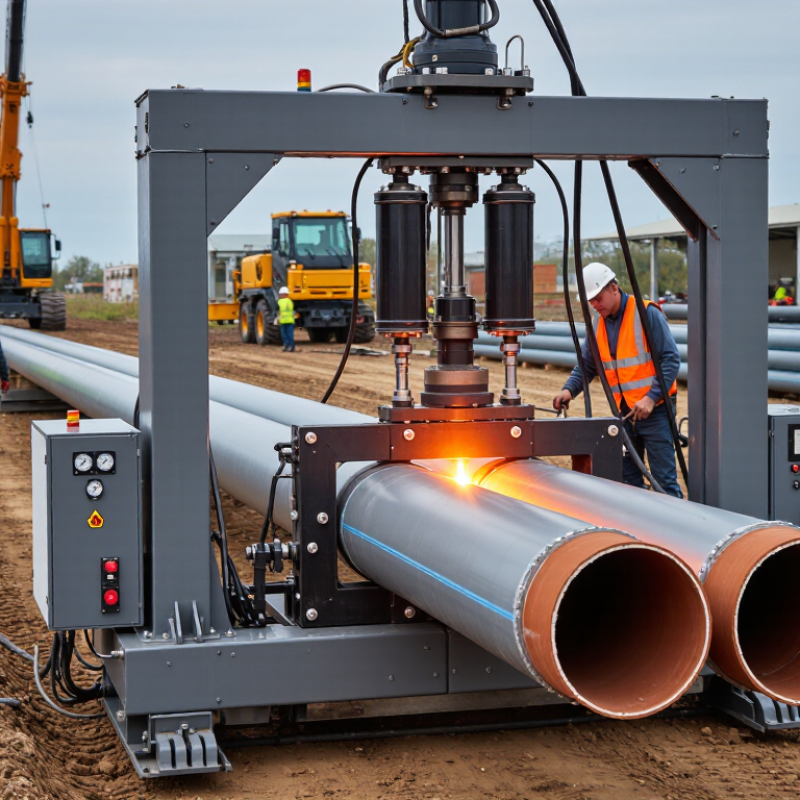
Table of Contents [Hide]
What Is a Fusion Pipe Welder and How Does It Work?
A fusion pipe welder joins thermoplastic pipes, usually polyethylene or polypropylene, through controlled heat and pressure. It does not use glue, threads, or metal fittings. The machine clamps both pipe ends, aligns them, and presses them against a heated plate. The softened faces then meet under pressure and cool into one continuous joint.
The process has four practical stages: alignment, heating, joining, and cooling. ISO 21307 describes three butt-fusion procedures, including low-pressure and high-pressure methods. ASTM F2620 also links reliable joints to correct temperature, interface pressure, and cooling time. These settings depend on pipe material, wall thickness, and diameter. Guesswork is risky.
The U.S. EPA’s 2023 Drinking Water Infrastructure Needs Survey estimated a national need of 625 billion dollars over 20 years. That pressure increases interest in durable, repairable pipe systems. The Plastics Pipe Institute’s field guidance stresses clean surfaces, stable clamping, and documented fusion parameters. A strong bead helps, but it is not complete proof of quality. I would not trust a rushed visual inspection alone. Moisture, wind, poor alignment, or early movement can weaken the joint invisibly. Experienced technicians record heater temperature, drag pressure, bead appearance, and cooling time. The best fusion pipe welder is therefore the one that matches the pipe system, follows recognized procedures, and gives operators precise control.
What Is the Best Fusion Pipe Welder? - What Is a Fusion Pipe Welder and How Does It Work?
| Welder Type | How It Works | Typical Pipe Size Range | Common Heating or Fusion Method | Typical Operating Temperature | Joint Characteristics | Best Use | Main Advantages | Important Limitations |
|---|---|---|---|---|---|---|---|---|
| Socket Fusion Welder | The outside of the pipe and the inside of a fitting are heated at the same time, then pushed together while the surfaces are molten. | About 16–125 mm, depending on the tool and applicable standard. | Heated male and female dies create a socket-and-spigot joint. | Usually around 200–260°C for thermoplastic pipe materials; the exact setting depends on the material and procedure. | Compact, fitting-based joint with no separate filler material. | Small-diameter water, irrigation, compressed-air, and process-piping installations. | Portable, comparatively affordable, fast to set up, and suitable for confined areas. | Limited to smaller sizes; requires accurate insertion depth, alignment, and heating time. |
| Butt Fusion Welder | Two pipe ends are aligned, faced flat, heated against a plate, and pressed together under controlled pressure until the joint cools. | Commonly about 40–2,000 mm; the practical range depends on machine capacity. | A heated plate softens the matching pipe ends before controlled end-to-end joining. | Often approximately 200–240°C for polyethylene pipe, subject to material and standard requirements. | Continuous homogeneous joint with a visible fusion bead when correctly made. | Medium- and large-diameter polyethylene pipelines, utilities, and industrial systems. | Strong, reliable joints; no fittings are required for straight runs; suitable for long pipeline sections. | Needs a stable work area, accurate alignment, hydraulic or mechanical force, and trained operation. |
| Electrofusion Welder | An electrically heated wire embedded in a special fitting melts the fitting and pipe surfaces to form a fused connection. | Commonly about 20–630 mm, with the actual range determined by fitting design and equipment. | Electrical resistance wires in the fitting generate controlled heat. | The fitting’s barcode, instructions, or procedure normally determines the fusion cycle rather than a manually selected temperature. | Fitting-based joint that can be used for couplers, tees, reducers, repairs, and service connections. | Repairs, tie-ins, restricted-access areas, and complex polyethylene pipeline layouts. | Works in confined spaces; does not require a large external heating plate; supports many fitting configurations. | Requires compatible electrofusion fittings, clean and properly scraped pipe surfaces, power, and controlled cooling. |
| Saddle Fusion Welder | A pipe surface and a saddle fitting are heated with matching tools, then pressed together to create a branch connection. | Often used on mains from about 63 mm upward, with branch sizes commonly selected from approximately 20–125 mm. | Heated concave and convex tools soften the pipe wall and saddle base before joining. | Typically follows the material-specific fusion procedure, commonly within the heating range used for polyethylene fusion. | Branch or service connection made directly onto the main pipe. | Service lines, branch connections, irrigation systems, and polyethylene distribution networks. | Creates a branch without cutting out a section of the main pipe; useful for network extensions. | Requires careful positioning and clamping; not intended for ordinary straight-line pipe joining. |
| Multi-Function Fusion Machine | Uses interchangeable clamps, heating plates, and tooling to perform more than one fusion process. | Usually about 20–630 mm, although some systems cover larger sizes with additional tooling. | May support socket, butt, saddle, or specialized fusion operations depending on the attachments. | Controlled according to the selected material, tool, and fusion procedure. | Joint quality depends on the selected process and the accuracy of the machine setup. | Contractors and maintenance teams handling varied pipe sizes and connection types. | Versatile, reduces the need for several separate machines, and can improve equipment utilization. | Higher purchase cost, more setup decisions, and potentially greater weight and maintenance requirements. |
Technical ranges are typical industry values and can vary by pipe material, wall thickness, fitting design, applicable standard, and equipment model. Correct fusion requires proper surface preparation, alignment, heating or electrical-cycle control, joining pressure, and cooling time.